

Quick Summary
Rack grounding connects the server rack frame to the building's earth electrode so fault current has a safe path to ground. Bonding ties every metal part of the rack together at the same electrical potential. Both are needed, and the power cable's earth pin alone does not bond the rack reliably.
- Earthing connects the rack to the building earth electrode so fault current has a path to ground.
- Bonding connects all metal parts of the rack so they sit at the same electrical potential.
- The rack frame, doors, side panels, cable trays and PDU chassis all need a reliable connection.
- Scrape paint or coating off bonding points before fitting the lead, since it blocks electrical contact.
- Test continuity from each metal part back to the earth point and record every reading.
Table of Contents
- Why Server Rack Grounding and Bonding Matter
- Server Rack Earthing Requirements: What Must Be Connected
- Grounding Through the Power Cable Is Not Enough
- Installing the Rack Bonding Jumper Correctly
- Building the Equipotential Bonding Connection Step by Step
- Testing Server Cabinet Earth Continuity
- Server Rack Installation Checklist for Grounding and Bonding
- Booking Your Rack Earthing Inspection and Commissioning With Treske
- Frequently Asked Questions
Server Rack Grounding and Bonding: A Step-by-Step Guide
Last Updated: November 7, 2026
Why Server Rack Grounding and Bonding Matter
Rack grounding keeps people and equipment safe when a fault happens. Rack earthing is installed and commissioned by qualified teams, and the same basic checks apply on every site.
A common mistake is treating the rack as "just a cabinet." It is part of the building's earthing system, and it needs to be treated that way from the first bolt.
Watch out: a rack with painted or powder-coated mounting faces can look bonded while the paint blocks the electrical contact.
Server Rack Earthing Requirements: What Must Be Connected
The rack frame, every metal panel and door, the cable tray, and the PDU chassis all need a reliable connection to the earthing system.
Many installers find that the frame is the easy part. The doors, side panels and removable trays are where connections go missing.
- Rack frame and mounting rails
- Doors and removable side panels
- Cable trays and cable ladder
Our Vertiv VE Series racks are built for this kind of installation, and the frame gives you a clear bonding surface to work from. For the broader set of racks in our range, see the Vertiv VE Series Server Racks.

Where a rack has a metal base plate or floor-standing feet, check that the earthing point is clean and reachable before the rack is moved into position.
For larger floor-standing cabinets, the Schneider Electric NetShelter SX 42U Floor Standing Rack Cabinet is one example of a model with a clearly defined earthing point and generous internal space for cable management.

Assess the rack before you bond it
Before you fit a single jumper, walk the rack and record what is actually there. A repeatable rack-level assessment catches the parts that drawings and handover packs miss, especially in racks that have been modified by several contractors over time.
- Photograph the rack from front, rear and both sides, including the top and base.
- List every removable metal part: doors, side panels, roof panels, blanking panels, cable trays, brush strips and earthing brackets.
- Identify unknown devices by label, MAC address or management interface, and record what each one is bonded to, or note that it is not bonded at all.
- Record dependencies: which devices share a PDU, which trays carry which cables, and which parts are removed during routine service.
- Assign an owner for each rack so the bonding record has a responsible person, not just a file reference.
A common pattern is to find doors bonded on one hinge and side panels not bonded at all, because a panel was swapped during a repair and the link was not refitted.
Mixed-generation racks need mixed-generation checks
Legacy and modern equipment often share the same cabinet, and the earthing requirements do not disappear because the hardware is old. Checking compatibility at each bonding point reinforces grounding and bonding principles that keep legacy and modern equipment safely connected.
- Rails and form factors: older rails may not provide a clean metal-to-metal path to the frame. Confirm the rail is bonded to the frame, not just bolted to a painted surface.
- Connectors and lugs: legacy equipment may use different lug sizes or terminal types. Use a listed lug that matches the conductor and the terminal, and do not mix dissimilar metals without a suitable connector.
- Voltage and power interfaces: confirm the PDU chassis is bonded and that the earth pin of each outlet is continuous to the PDU chassis earth.
Watch out: a rack that mixes powder-coated legacy panels with modern bonded panels can look fully bonded while the legacy panels sit at a different potential.
Thermal and power context for the bonding plan
Bonding does not happen in isolation. Heat, airflow and power draw affect where you can safely run jumpers and how much space you have to work at the earth point.
- Check the heat output of older equipment before you pack the rack. High-heat legacy units can cook insulation on bonding conductors run too close to exhaust airflow.
- Keep bonding jumpers clear of airflow paths and fan intakes so they are not disturbed during service.
- Confirm the circuit capacity and PDU rating before adding equipment, and record the power draw per rack so the earthing design matches the actual load.
These checks are not a substitute for the electrical installation standard, but they stop the most common physical conflicts between bonding work and the rest of the rack build.
Grounding Through the Power Cable Is Not Enough
A very common assumption is that the power cable's earth pin will ground the rack. It will not, at least not reliably on its own.
The earth pin in a power lead only carries current from the equipment it feeds. It does not bond the rack frame, doors and trays together.
Treat the power-cable earth as one layer in a system of protection, not the whole system.
Installing the Rack Bonding Jumper Correctly
A rack bonding jumper is a short conductor that links the rack frame to the earthing point. Use a green-and-yellow conductor of the size specified by the installation standard for your site.
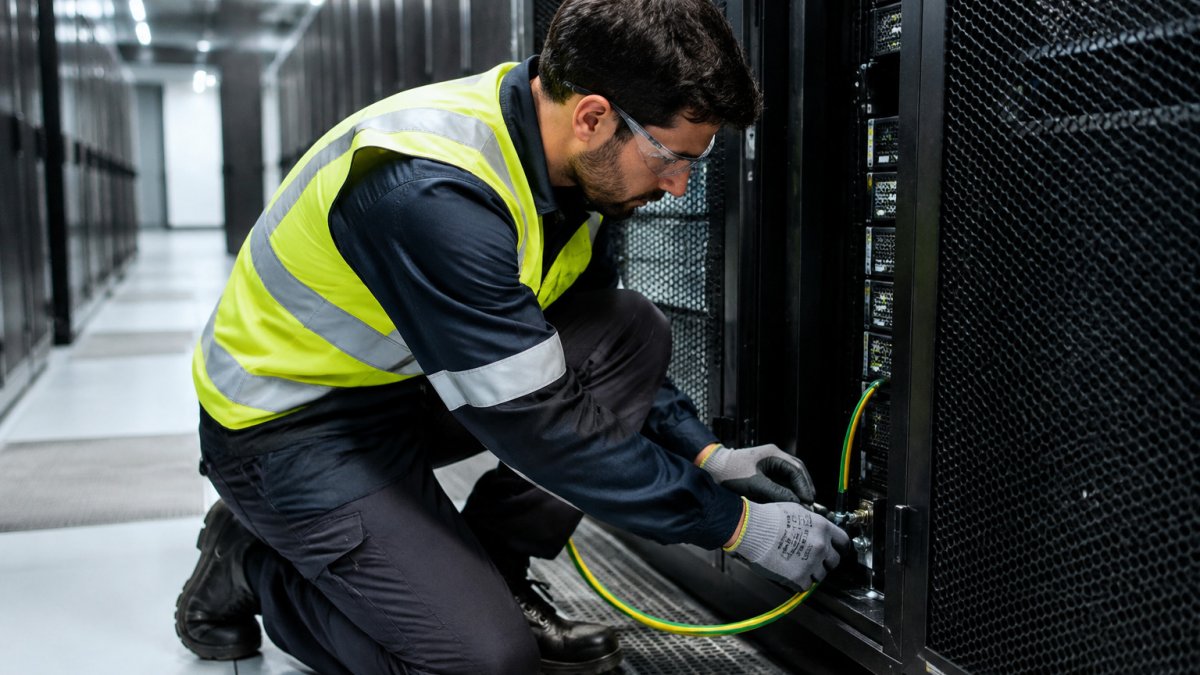
Follow these steps:
- Power off and isolate the rack before you start work.
- Remove any paint or coating from the bonding point on the rack frame.
- Attach the jumper using a listed lug and a bolt that is tightened to the correct torque.
- Run the jumper to the building earth bar or the designated earthing point.
- Label the connection so the next technician can see it.
Keep the jumper short and direct. Loops and sharp bends add resistance and make the connection harder to test later.
!Electrician attaching a bonding lead to a server cabinet earthing point in a data centre aisle, cabinet earthing point in focus
The article's core installation steps for the bonding jumper come down to a few key details:
Step |
What to do |
Note |
|---|---|---|
Isolate |
Power off and isolate the rack |
Before any work starts |
Clean |
Remove paint or coating at the bonding point |
Paint blocks electrical contact |
Attach |
Fit jumper with listed lug and correct torque |
Use green-and-yellow conductor |
Run |
Connect to building earth bar or earthing point |
Keep the jumper short and direct |
Label |
Mark the connection |
So the next technician can see it |
Building the Equipotential Bonding Connection Step by Step
Equipotential bonding ties every metal part of the rack and the surrounding infrastructure to one reference point. The aim is to stop voltage differences between parts that a person might touch at the same time.
Here is a practical sequence:
- Identify the main earth bar for the room or row.
- Bond the rack frame to that bar with the jumper from the previous section.
- Bond each door, side panel and tray with its own short link.
- Bond any metal enclosure or PDU chassis inside the rack.
- Check every link before you close the cabinet.
For high-density racks, this step takes longer than most people expect. Plan an hour or more for a fully loaded rack with multiple doors and trays.
Testing Server Cabinet Earth Continuity
Once the bonding is complete, test the continuity from each metal part back to the earth point.
A useful practice is to test from the frame, then from each door and tray, and note any reading that looks high compared with the others.
Keep the test results with the rack's commissioning records. If an inspection happens later, those records show exactly what was tested and when.
The earthing checks in this section are the same ones our commissioning team runs during site acceptance testing-style audits, and the results feed directly into the handover documents.
Server Rack Installation Checklist for Grounding and Bonding
Use this checklist before you sign off any rack installation:
- Rack frame bonded to the designated earth point
- Every door bonded with its own link
- Cable trays and ladders bonded
Many teams find it useful to print this list and attach it to the rack during installation. That way, nobody has to remember the steps from memory.
For the wider rack setup, our Eaton RE Series Racks include the accessories and mounting points you will need for a clean installation.
Change control and rollback for bonding work
Bonding changes are electrical changes, and they deserve the same change control as any other work on a live rack. A low-risk procedure keeps the rack serviceable if something goes wrong.
- Define the maintenance window. Bonding work on a live rack should be scheduled when the equipment can be isolated or when the work is limited to parts that can be safely removed.
- Back up configuration and records. Photograph the existing bonding before you change it, and export any device configuration that depends on the rack earth reference.
- Test dependencies first. Confirm which devices share a PDU or earth bar, and check that isolating one part does not remove the earth path for another.
- Set rollback criteria. If continuity readings are worse after the change, or if a device fails to power up, stop and restore the previous bonding arrangement before continuing.
- Validate after the change. Re-test continuity from every metal part, record the readings, and compare them with the pre-change baseline.
Watch out: removing a door or side panel to reach a bonding point can break the earth path for equipment mounted on that panel. Bond the replacement part before you remove the original, or isolate the equipment first.
Security controls for hardware that cannot be patched
Legacy equipment often cannot be patched, and bonding work is a good moment to review the compensating controls around it. The earthing system is part of the physical security boundary, not separate from it.
- Network segmentation: place unpatched devices on a segmented network with restricted access, and document which devices are in scope.
- Restricted physical access: lock the rack, control keys, and record who has access to the earth bar and bonding points.
- Monitoring: monitor for tampering with bonding conductors and for unauthorised equipment added to the rack.
These controls do not replace patching, but they reduce the exposure of hardware that cannot be updated and give the site a defensible record if an audit occurs.
Measurable sign-off thresholds
A checklist is only useful if each item has a pass condition. Record the following at sign-off so the next technician can compare against a baseline rather than a memory.
- Continuity reading for each bonded part, recorded with the instrument used and the date.
- Visual confirmation that paint has been removed at every bonding point.
- Label present and legible on every bonding connection.
A common pattern is for readings to drift upward between services because a lug has corroded or a bolt has loosened. Comparing against the sign-off baseline is what turns a checklist into a maintenance tool.
Booking Your Rack Earthing Inspection and Commissioning With Treske
If you want a qualified team to check your grounding and bonding, Treske Pty Limited can be contacted about inspection and commissioning services for critical infrastructure.
Our team is one of the reasons many sites choose to meet the Treske team before booking work, so you can see who will be on site and what they are qualified to do.
Frequently Asked Questions
Does a server rack need to be grounded?
Yes. Metal server racks and cabinets must be connected to the earthing system so that fault current has a low-impedance path back to the switchboard and a stray voltage cannot build up on the enclosure. Grounding protects people who touch the rack and helps protective devices operate quickly during a fault. The exact arrangement should follow AS/NZS 3000 (the Wiring Rules) and the design of the installation, so have a licensed electrician confirm the connection points for your site before any equipment is energised.
What is the difference between grounding and bonding a server rack?
Grounding connects the rack to the earth of the electrical installation, providing a safe path for fault current. Bonding connects the rack's metal parts to each other and to other conductive items, such as cable trays, raised floor grids and the equipotential bonding network, so they sit at the same potential. Both are needed. A rack can be earthed but poorly bonded, leaving voltage differences between adjacent metalwork.
How do you test continuity on a bonded server rack?
Continuity testing measures the resistance between the rack frame and the earthing point using a low-resistance ohmmeter, with the supply isolated. Test each bonded component back to the bonding bar and record the readings against the design values. Readings should be low and consistent across all points. Any high or open reading means a loose connection, corrosion or a broken conductor, and it must be fixed and retested before commissioning.
Who should inspect server rack grounding and bonding?
The installation should be carried out and certified by a licensed electrician who is competent in earthing and bonding under AS/NZS 3000. Independent verification, such as site acceptance testing, adds confidence before handover. Treske provides design, supply and installation of power, cooling and rack enclosure systems for critical infrastructure in Australia and New Zealand, and records from each inspection should be kept with the facility's asset documentation.
